 EN
 CN
 ES
 AR
 FR
 PT
 RU
 KO
 JA
 DE



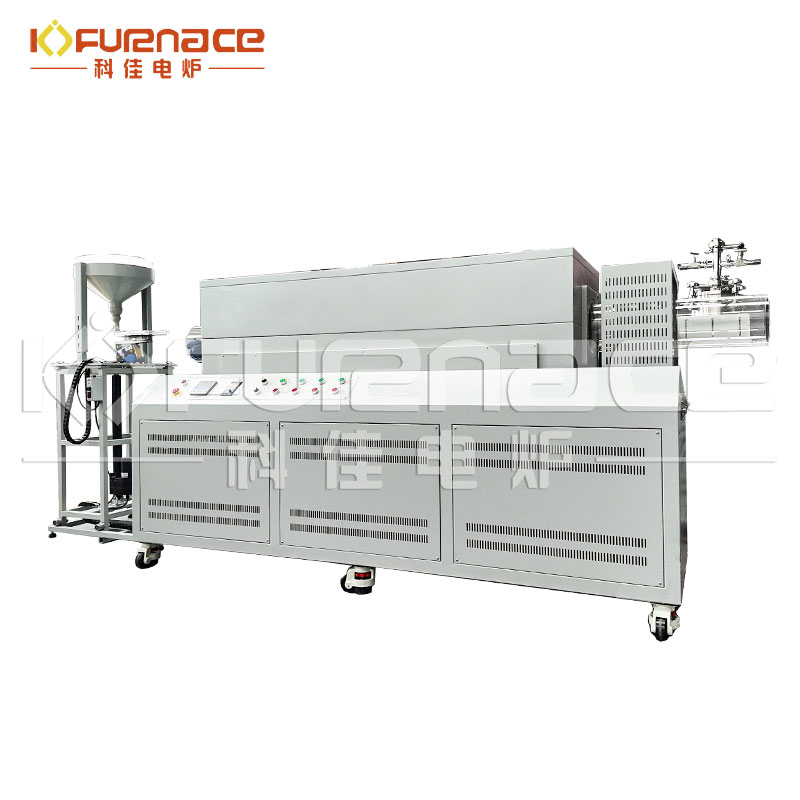
Tube Furnace Annealing: Atmosphere and Ramp Rate Effects on Grain Size
Posted on:2026-10-27 13:39:24
1. Overview of Tube Furnace Annealing and Grain Evolution Mechanism
1.1 Annealing Core Purpose and Tube Furnace Process Advantages
Tube furnace annealing realizes precise atmosphere switching and segmented temperature programming, which is the mainstream thermal process for regulating grain structure, eliminating residual stress and optimizing material properties of metals and ceramics.
Annealing is a key heat treatment process for metal alloys, oxide ceramics, non-oxide ceramics and cermet materials. By heating to the target temperature, holding and controlled cooling, the deformed lattice recovers, recrystallization occurs, and grain growth or grain refinement is realized. Horizontal/vertical tube furnaces feature sealed tube cavity, independent gas path, multi-zone PID temperature control and programmable ramp curve, which can stably realize inert, oxidizing, reducing, vacuum and mixed atmosphere annealing. Compared with box furnaces, tube furnaces have better atmosphere uniformity, lower gas consumption and more stable oxygen partial pressure, which is suitable for laboratory material development and small-batch precision industrial annealing. The final grain morphology, grain size distribution and grain boundary state are mainly determined by three core variables: annealing atmosphere, heating rate and cooling rate.
1.2 Basic Principle of Grain Recrystallization and Grain Growth
Metals rely on deformation storage energy to drive recrystallization and grain boundary migration; ceramics rely on ion vacancy diffusion and grain boundary migration to realize grain growth. Atmosphere and ramp rate jointly control diffusion kinetics and defect concentration.
For deformed metal materials, the driving force of annealing recrystallization comes from the stored strain energy after cold working. New dislocation-free grains nucleate and grow to replace the original deformed fibrous structure. For ceramics, the driving force of grain growth comes from the reduction of grain boundary area and interfacial energy, and the growth rate depends on cation/anion diffusion rate at grain boundaries. The Ostwald ripening effect will appear during long-term heat preservation: large grains swallow small grains and form abnormal grain growth. Atmosphere changes the lattice vacancy concentration and oxidation-reduction state; heating rate determines the starting temperature of recovery and recrystallization; cooling rate affects the phase transformation and residual stress after annealing, and indirectly locks the final grain structure.
1.3 Industrial Pain Points of Annealing Parameter Matching
Improper atmosphere or unreasonable ramp rate often leads to abnormal grain coarsening, uneven grain size, surface oxidation, phase transition and residual stress cracking, which deteriorates mechanical, electrical and thermal properties.
Many users only focus on annealing temperature and holding time, ignoring atmosphere and ramp rate. In metal annealing, fast heating may cause local overheating and mixed grain structure; slow heating leads to excessive recovery, insufficient recrystallization driving force and coarse grains. In ceramic annealing, reducing atmosphere increases oxygen vacancies and accelerates grain boundary diffusion, which easily triggers abnormal grain growth; oxidizing atmosphere may introduce surface oxide layers and pin grain boundaries. The mismatch of cooling rate will cause thermal stress and even phase transformation. This article separately analyzes the influence logic of atmosphere and ramp rate on metal and ceramic grains, and provides a scenario-based parameter matching scheme for tube furnace annealing.
2. Influence of Annealing Atmosphere on Grain Evolution of Metals and Ceramics
2.1 Oxidizing Atmosphere (Air / O₂): Grain Boundary Pinning and Surface Oxidation
Oxidizing atmosphere forms oxide precipitates on the surface and grain boundaries, produces Zener pinning effect, inhibits grain boundary migration and restrains excessive grain growth; but it may cause metal surface oxidation and ceramic phase change.
When metals are annealed in air or oxygen, the surface and grain boundaries preferentially form oxide films or dispersed oxide particles. These oxide particles pin the grain boundaries and slow down the migration rate of grain boundaries, so the grains are finer and the grain size distribution is more uniform. However, for precision alloy parts, excessive oxidation will form thick oxide scales, introduce surface defects and reduce the mechanical properties. For oxide ceramics such as zirconia, high oxygen partial pressure stabilizes the tetragonal phase and suppresses the phase transformation induced grain growth; for non-oxide ceramics such as SiC and Si₃N₄, oxidizing atmosphere will generate SiO₂ glass phase at grain boundaries, change the grain boundary viscosity and diffusion rate, and significantly change the grain growth kinetics.
2.2 Inert Atmosphere (Ar / N₂): Low Oxygen Partial Pressure, Stable Baseline Grain Growth
Inert atmosphere avoids obvious oxidation or reduction, grain growth follows the intrinsic diffusion rule of the material, and it is the preferred atmosphere for obtaining stable and repeatable grain structure.
High-purity argon or nitrogen is the most widely used annealing atmosphere in tube furnaces. The oxygen partial pressure in the cavity is controlled at a low level, and the material basically maintains its original stoichiometric ratio. For cold-rolled metals, recrystallization and grain growth proceed naturally without the interference of oxide pinning or reduction dissolution. For most oxide ceramics, inert atmosphere is between oxidation and reduction, and the grain growth rate is moderate, which is convenient for stable process debugging. Attention should be paid to the residual oxygen and water vapor in the tube. If the sealing and purging are not in place, trace oxygen will still cause surface oxidation and grain boundary pinning, resulting in inconsistent grain size between batches.
2.3 Reducing Atmosphere (H₂ / H₂-Ar Mixed Gas): Accelerate Diffusion and Easily Trigger Abnormal Grain Growth
Reducing atmosphere reduces oxides and increases lattice oxygen vacancies, accelerates grain boundary diffusion, significantly improves grain growth rate; it is suitable for deoxidation of metal matrix, but high risk of abnormal grain coarsening for ceramics.
Hydrogen-containing mixed atmosphere can reduce surface oxides and grain boundary oxide precipitates of metals, remove pinning particles, release grain boundary migration ability, and the grains tend to grow larger. For nickel-based, copper-based and iron-based alloy annealing, reducing atmosphere is used to bright annealing and obtain clean grain boundaries. For oxide ceramics such as barium titanate and YSZ, low oxygen partial pressure increases oxygen vacancy concentration, the cation diffusion rate at grain boundary is greatly improved, and the grain growth speed is obviously accelerated. If the holding time is not strictly controlled, abnormal grain growth will occur, and a small number of oversized grains will appear in the fine grain matrix, which seriously reduces the material toughness and uniformity.
2.4 Vacuum Atmosphere: Ultra-Low Oxygen Partial Pressure, Suitable for Active Metal and Non-Oxide Ceramic Annealing
High vacuum minimizes oxygen pollution, avoids oxidation of active metals such as titanium and tantalum; the diffusion mechanism is similar to reducing atmosphere, and the grain growth rate is higher than that in air.
Vacuum annealing of tube furnace is suitable for easy-to-oxidize metals, amorphous alloys and non-oxide ceramics. The oxide layer on the surface can be decomposed and volatilized under high temperature and vacuum. Without oxide pinning, the grain boundary migration resistance is low. It is easy to obtain coarse grains under long-time high-temperature holding. The disadvantage of vacuum annealing is that the volatile elements in the material are easy to lose, resulting in composition deviation and abnormal grain evolution. It is necessary to balance vacuum degree, temperature and holding time according to the material system.
3. Heating & Cooling Rate: Control Recovery, Recrystallization Nucleation, Grain Growth, Phase Transformation and Residual Stress
3.1 Slow Heating Rate (0.5–2 ℃/min): Sufficient Recovery, Low Recrystallization Driving Force, Easy to Form Coarse Grains
Slow heating provides sufficient time for dislocation recovery, consumes deformation storage energy, reduces recrystallization nucleation density, and finally forms large and uniform grains.
For cold-deformed metals, slow heating makes the dislocation rearrange and recover in the low-temperature section before reaching the recrystallization temperature. The stored energy, which is the driving force for recrystallization, is consumed in advance. The number of new crystal nuclei formed at the recrystallization temperature is small, and the grains have enough time to grow up, showing large grain size and good uniformity. For ceramics, slow heating makes the temperature field inside the blank uniform, avoids local hot spots, and the grain grows steadily along the grain boundary diffusion path. Slow heating is suitable for materials that need large grain structure, such as soft magnetic alloys, high thermal conductivity ceramics; but it is not suitable for materials that pursue fine grain strengthening.
3.2 Medium Heating Rate (2–10 ℃/min): Balanced Nucleation and Growth, Most Widely Used Process Window
Medium heating rate retains part of the deformation driving force, the recrystallization nucleation density is moderate, the grain size is uniform and controllable, which is the conventional preferred parameter for tube furnace annealing.
Most tube furnace annealing processes adopt 2–10 ℃/min heating rate. It can avoid excessive recovery caused by too slow heating and uneven grain size caused by ultra-fast heating. The temperature gradient inside the sample is small, the thermal stress is low, and the risk of cracking of brittle ceramics is reduced. This interval is convenient for process adjustment: by matching different holding time, fine grain or medium grain structure can be obtained. It is widely used in stainless steel, aluminum alloy, alumina, zirconia and other material systems, and has good repeatability for batch production.
3.3 Fast / Ultra-Fast Heating Rate (>10 ℃/min): Suppress Recovery, High Nucleation Density, Obtain Fine Grains, Risk of Mixed Grains
Rapid heating skips the low-temperature recovery stage, retains high deformation storage energy, increases recrystallization nucleation rate, and obtains fine grains; but excessive heating rate easily causes temperature gradient and mixed grain structure.
Ultra-fast heating makes the sample quickly cross the recovery temperature range, the dislocation structure is retained, and the driving force for recrystallization is high. A large number of new crystal nuclei are formed instantaneously, and the grain growth time is insufficient, so the final grain is refined. This process is often used for fine-grained strengthening of metal alloys. However, too fast heating will bring obvious internal temperature gradient. The surface reaches the recrystallization temperature first, while the center is still in the recovery state. The difference of recrystallization sequence leads to mixed grain structure with large and small grains coexisting. For ceramics with poor thermal conductivity, rapid heating is easy to induce thermal stress cracking.
3.4 Slow Furnace Cooling: Sufficient Grain Growth, Low Residual Stress, Stable Equilibrium Microstructure
Slow cooling allows grains to continue to grow slightly in the high-temperature section, releases thermal stress, and obtains equilibrium phase and stable grain structure; it is suitable for stress-sensitive ceramics and brittle alloys.
Furnace cooling is the most common cooling mode of tube furnace annealing. After heat preservation, the power is cut off and the temperature drops naturally with the furnace. In the high-temperature slow cooling section, grain boundary diffusion continues, and the grains have a small amount of secondary growth. The temperature difference between the inside and outside of the sample is small, the thermal stress is released slowly, and the probability of cracking of ceramic samples is greatly reduced. The disadvantage is that for some metastable phase systems, slow cooling will induce phase transformation and change the grain structure formed at high temperature.
3.5 Controlled Medium Cooling Rate: Balance Stress and Grain Size, Convenient for Microstructure Locking
Programmed medium cooling can suppress excessive grain growth in the high-temperature zone, while avoiding excessive thermal shock, and is suitable for multi-stage annealing with strict grain size requirements.
By setting a fixed cooling rate of 1–5 ℃/min in the tube furnace program, the high-temperature grain structure can be quickly locked before the grain continues to grow. It avoids the long-time high-temperature residence of furnace cooling and prevents further grain coarsening. Combined with atmosphere protection, this method is widely used in functional ceramics, precision metal parts that require stable grain size and low residual stress.
3.6 Rapid Cooling / Gas Quenching: Suppress Grain Growth, Retain High-Temperature Microstructure, High Stress Risk
High-speed gas quenching rapidly passes through the high-temperature grain growth zone, freezes the grain state at the annealing temperature, and obtains fine grains; the temperature gradient is large, which is easy to introduce residual stress and cracks.
Tube furnaces equipped with rapid gas quenching function can inject high-flow protective gas to realize rapid cooling. The residence time in the high-temperature grain growth interval is extremely short, and the grain basically no longer grows during cooling, which can retain the fine grain structure formed at the annealing temperature. It is commonly used for metal alloys that need to retain high-temperature recrystallized structure. However, rapid cooling will produce huge temperature gradient inside thick samples. For ceramics, cermets and brittle materials, it is easy to crack. It is necessary to strictly control the gas flow rate and segment the cooling curve.
4. Material Classification and Process Parameter Matching Guide
4.1 Metal Materials (Alloy, Cold-Rolled Metal, Amorphous Alloy)
Fine-grained strengthening: inert / reducing atmosphere + fast heating + medium cooling; soft magnetic large grain: inert atmosphere + slow heating + furnace cooling; bright stress relief annealing: hydrogen reducing atmosphere + medium heating + slow cooling.
Cold-rolled aluminum alloy, copper alloy and stainless steel: if fine grain and high strength are required, adopt Ar atmosphere, heating rate 5–10 ℃/min, controlled cooling; if softening and high plasticity are required, slow heating 1–2 ℃/min and furnace cooling. Nickel-based alloy, high-temperature alloy bright annealing: dilute hydrogen argon mixed atmosphere, strictly control dew point, medium heating rate to avoid surface oxidation and abnormal grain growth. Amorphous alloy annealing: low vacuum or inert atmosphere, medium and low heating rate, avoid over-annealing crystallization and grain coarsening.
4.2 Oxide Ceramics (Al₂O₃, ZrO₂, BaTiO₃, YSZ)
Dense fine-grained ceramics: oxidizing / inert atmosphere + medium heating rate + slow cooling; reducing atmosphere annealing needs to shorten holding time to suppress abnormal grain growth.
Alumina, zirconia structural ceramics mostly adopt air or argon atmosphere, heating rate 1–5 ℃/min, furnace cooling, to obtain uniform grain and low stress. For dielectric ceramics such as barium titanate used in MLCC, reducing atmosphere is required for co-firing with nickel electrodes. At this time, the oxygen vacancy concentration rises, the grain growth is accelerated, and the holding time must be shortened to prevent individual grains from being abnormally large. Zirconia needs to control oxygen partial pressure to stabilize the tetragonal phase and avoid phase transformation and grain growth during cooling.
4.3 Non-Oxide Ceramics and Cermet (SiC, Si₃N₄, Metal-Ceramic Composite)
Non-oxide ceramics must use inert or vacuum atmosphere; reducing atmosphere should be used cautiously. Medium heating rate and segmented cooling are adopted to balance grain growth and anti-oxidation.
SiC and silicon nitride ceramics are easy to oxidize in air above 1000 ℃, so they must be annealed in high-purity argon or vacuum. The grain boundary is controlled by the sintering aid glass phase, and the heating rate cannot be too fast to prevent thermal cracking. For cermet such as Ni-YSZ, reducing atmosphere will promote the growth of metal phase particles and ceramic grains at the same time. The atmosphere oxygen partial pressure, temperature and holding time must be matched synchronously to avoid the mismatch of grain size between metal phase and ceramic phase.
5. Common Defect Troubleshooting and Annealing Curve Optimization
5.1 Mixed Grain, Abnormal Coarse Grain
Main causes: uneven heating rate, unstable atmosphere oxygen partial pressure, excessive holding time in reducing atmosphere; solutions: stabilize gas flow, reduce holding time, adopt segmented heating.
Mixed grains are one of the most common annealing defects. The root cause is the asynchronous recrystallization or uneven grain boundary migration rate. It is necessary to check whether the tube furnace has temperature gradient in the hot zone, whether the gas purging is sufficient before heating, and whether the hydrogen flow is too high. A segmented heating curve can be set: low-temperature preheating and heat preservation to homogenize the temperature field, then heat up to the target annealing temperature at a medium rate, and shorten the high-temperature holding time in reducing atmosphere.
5.2 Surface Oxidation, Discoloration and Grain Boundary Pollution
Main causes: insufficient purging, sealing leakage, residual oxygen in the tube; solutions: increase pre-purging time, check O-ring and flange sealing, use high-purity protective gas.
Even under inert gas, trace oxygen and water vapor will cause surface oxidation of metals and form impurity phases at ceramic grain boundaries, which will pin grain boundaries and make the grain size smaller than the expected value. Before annealing, the tube cavity needs to be purged for 3–5 times to replace the air. For high-demand bright annealing, a gas dew point detector is recommended to monitor the water vapor content in the atmosphere.
5.3 Thermal Stress Cracking of Ceramic Samples
Main causes: too fast heating or cooling rate, large sample thickness; solutions: add low-temperature preheating section, reduce ramp rate, avoid direct gas quenching of thick ceramic blanks.
Ceramic materials have low thermal conductivity and poor thermal shock resistance. Thick samples must be equipped with a long preheating section below 600 ℃ with a slow ramp rate. It is forbidden to directly use rapid gas quenching. If rapid cooling is required, segmented cooling is adopted: slow cooling in the high-temperature section above the phase transition point, and appropriately increase the cooling rate after the temperature drops to the low-temperature safe zone.
6. Summary and Process Design Suggestions
6.1 Core Law of Atmosphere and Ramp Rate on Grain Regulation
Atmosphere determines the diffusion driving force and grain boundary pinning state from the chemical level; ramp rate controls the recrystallization nucleation and grain growth time window from the kinetic level. The two are coupled together to determine the final grain structure.
Atmosphere is the chemical regulation knob of annealing: oxidizing atmosphere is easy to form pinning phase and refine grains; reducing / vacuum atmosphere increases vacancies, accelerates diffusion and promotes grain growth. The heating and cooling rate is the kinetic regulation knob: slow heating + slow cooling is conducive to grain growth and stress relief; fast heating + rapid cooling is conducive to grain refinement and locking high-temperature microstructure. There is no universal optimal parameter, and the material system and performance target must be the first priority.
6.2 Suggestions for Tube Furnace Annealing Process Development
When developing the annealing process, first lock the atmosphere according to the material anti-oxidation and phase stability requirements, then optimize the heating rate and holding time, and finally match the cooling curve.
The standard process development sequence is as follows: confirm the allowable atmosphere range of the material → set pre-purging parameters → formulate heating curve (preheating + formal heating) → determine annealing temperature and holding time → set cooling mode and cooling rate. For new materials, it is recommended to carry out gradient contrast experiments of atmosphere and ramp rate, and characterize the grain size by SEM / EBSD, so as to form a stable annealing process window. The multi-zone programmable tube furnace can realize more flexible segmented temperature and atmosphere switching, which is the preferred equipment for high-precision grain regulation.
Zhengzhou KJ Technology Co., Ltd. is a high-tech enterprise specializing in R&D and sales of heat treatment products, including muffle furnaces, tube furnaces, vacuum furnaces and more, widely used in metallurgy, ceramic sintering, battery materials, semiconductors, aerospace and other fields.
For inquiries and customized solutions, contact us via WhatsApp: +86 18037178440 or Email: web@kejiafurnace.com.
1.1 Annealing Core Purpose and Tube Furnace Process Advantages
Tube furnace annealing realizes precise atmosphere switching and segmented temperature programming, which is the mainstream thermal process for regulating grain structure, eliminating residual stress and optimizing material properties of metals and ceramics.
Annealing is a key heat treatment process for metal alloys, oxide ceramics, non-oxide ceramics and cermet materials. By heating to the target temperature, holding and controlled cooling, the deformed lattice recovers, recrystallization occurs, and grain growth or grain refinement is realized. Horizontal/vertical tube furnaces feature sealed tube cavity, independent gas path, multi-zone PID temperature control and programmable ramp curve, which can stably realize inert, oxidizing, reducing, vacuum and mixed atmosphere annealing. Compared with box furnaces, tube furnaces have better atmosphere uniformity, lower gas consumption and more stable oxygen partial pressure, which is suitable for laboratory material development and small-batch precision industrial annealing. The final grain morphology, grain size distribution and grain boundary state are mainly determined by three core variables: annealing atmosphere, heating rate and cooling rate.
1.2 Basic Principle of Grain Recrystallization and Grain Growth
Metals rely on deformation storage energy to drive recrystallization and grain boundary migration; ceramics rely on ion vacancy diffusion and grain boundary migration to realize grain growth. Atmosphere and ramp rate jointly control diffusion kinetics and defect concentration.
For deformed metal materials, the driving force of annealing recrystallization comes from the stored strain energy after cold working. New dislocation-free grains nucleate and grow to replace the original deformed fibrous structure. For ceramics, the driving force of grain growth comes from the reduction of grain boundary area and interfacial energy, and the growth rate depends on cation/anion diffusion rate at grain boundaries. The Ostwald ripening effect will appear during long-term heat preservation: large grains swallow small grains and form abnormal grain growth. Atmosphere changes the lattice vacancy concentration and oxidation-reduction state; heating rate determines the starting temperature of recovery and recrystallization; cooling rate affects the phase transformation and residual stress after annealing, and indirectly locks the final grain structure.
1.3 Industrial Pain Points of Annealing Parameter Matching
Improper atmosphere or unreasonable ramp rate often leads to abnormal grain coarsening, uneven grain size, surface oxidation, phase transition and residual stress cracking, which deteriorates mechanical, electrical and thermal properties.
Many users only focus on annealing temperature and holding time, ignoring atmosphere and ramp rate. In metal annealing, fast heating may cause local overheating and mixed grain structure; slow heating leads to excessive recovery, insufficient recrystallization driving force and coarse grains. In ceramic annealing, reducing atmosphere increases oxygen vacancies and accelerates grain boundary diffusion, which easily triggers abnormal grain growth; oxidizing atmosphere may introduce surface oxide layers and pin grain boundaries. The mismatch of cooling rate will cause thermal stress and even phase transformation. This article separately analyzes the influence logic of atmosphere and ramp rate on metal and ceramic grains, and provides a scenario-based parameter matching scheme for tube furnace annealing.
2. Influence of Annealing Atmosphere on Grain Evolution of Metals and Ceramics
2.1 Oxidizing Atmosphere (Air / O₂): Grain Boundary Pinning and Surface Oxidation
Oxidizing atmosphere forms oxide precipitates on the surface and grain boundaries, produces Zener pinning effect, inhibits grain boundary migration and restrains excessive grain growth; but it may cause metal surface oxidation and ceramic phase change.
When metals are annealed in air or oxygen, the surface and grain boundaries preferentially form oxide films or dispersed oxide particles. These oxide particles pin the grain boundaries and slow down the migration rate of grain boundaries, so the grains are finer and the grain size distribution is more uniform. However, for precision alloy parts, excessive oxidation will form thick oxide scales, introduce surface defects and reduce the mechanical properties. For oxide ceramics such as zirconia, high oxygen partial pressure stabilizes the tetragonal phase and suppresses the phase transformation induced grain growth; for non-oxide ceramics such as SiC and Si₃N₄, oxidizing atmosphere will generate SiO₂ glass phase at grain boundaries, change the grain boundary viscosity and diffusion rate, and significantly change the grain growth kinetics.
2.2 Inert Atmosphere (Ar / N₂): Low Oxygen Partial Pressure, Stable Baseline Grain Growth
Inert atmosphere avoids obvious oxidation or reduction, grain growth follows the intrinsic diffusion rule of the material, and it is the preferred atmosphere for obtaining stable and repeatable grain structure.
High-purity argon or nitrogen is the most widely used annealing atmosphere in tube furnaces. The oxygen partial pressure in the cavity is controlled at a low level, and the material basically maintains its original stoichiometric ratio. For cold-rolled metals, recrystallization and grain growth proceed naturally without the interference of oxide pinning or reduction dissolution. For most oxide ceramics, inert atmosphere is between oxidation and reduction, and the grain growth rate is moderate, which is convenient for stable process debugging. Attention should be paid to the residual oxygen and water vapor in the tube. If the sealing and purging are not in place, trace oxygen will still cause surface oxidation and grain boundary pinning, resulting in inconsistent grain size between batches.
2.3 Reducing Atmosphere (H₂ / H₂-Ar Mixed Gas): Accelerate Diffusion and Easily Trigger Abnormal Grain Growth
Reducing atmosphere reduces oxides and increases lattice oxygen vacancies, accelerates grain boundary diffusion, significantly improves grain growth rate; it is suitable for deoxidation of metal matrix, but high risk of abnormal grain coarsening for ceramics.
Hydrogen-containing mixed atmosphere can reduce surface oxides and grain boundary oxide precipitates of metals, remove pinning particles, release grain boundary migration ability, and the grains tend to grow larger. For nickel-based, copper-based and iron-based alloy annealing, reducing atmosphere is used to bright annealing and obtain clean grain boundaries. For oxide ceramics such as barium titanate and YSZ, low oxygen partial pressure increases oxygen vacancy concentration, the cation diffusion rate at grain boundary is greatly improved, and the grain growth speed is obviously accelerated. If the holding time is not strictly controlled, abnormal grain growth will occur, and a small number of oversized grains will appear in the fine grain matrix, which seriously reduces the material toughness and uniformity.
2.4 Vacuum Atmosphere: Ultra-Low Oxygen Partial Pressure, Suitable for Active Metal and Non-Oxide Ceramic Annealing
High vacuum minimizes oxygen pollution, avoids oxidation of active metals such as titanium and tantalum; the diffusion mechanism is similar to reducing atmosphere, and the grain growth rate is higher than that in air.
Vacuum annealing of tube furnace is suitable for easy-to-oxidize metals, amorphous alloys and non-oxide ceramics. The oxide layer on the surface can be decomposed and volatilized under high temperature and vacuum. Without oxide pinning, the grain boundary migration resistance is low. It is easy to obtain coarse grains under long-time high-temperature holding. The disadvantage of vacuum annealing is that the volatile elements in the material are easy to lose, resulting in composition deviation and abnormal grain evolution. It is necessary to balance vacuum degree, temperature and holding time according to the material system.
3. Heating & Cooling Rate: Control Recovery, Recrystallization Nucleation, Grain Growth, Phase Transformation and Residual Stress
3.1 Slow Heating Rate (0.5–2 ℃/min): Sufficient Recovery, Low Recrystallization Driving Force, Easy to Form Coarse Grains
Slow heating provides sufficient time for dislocation recovery, consumes deformation storage energy, reduces recrystallization nucleation density, and finally forms large and uniform grains.
For cold-deformed metals, slow heating makes the dislocation rearrange and recover in the low-temperature section before reaching the recrystallization temperature. The stored energy, which is the driving force for recrystallization, is consumed in advance. The number of new crystal nuclei formed at the recrystallization temperature is small, and the grains have enough time to grow up, showing large grain size and good uniformity. For ceramics, slow heating makes the temperature field inside the blank uniform, avoids local hot spots, and the grain grows steadily along the grain boundary diffusion path. Slow heating is suitable for materials that need large grain structure, such as soft magnetic alloys, high thermal conductivity ceramics; but it is not suitable for materials that pursue fine grain strengthening.
3.2 Medium Heating Rate (2–10 ℃/min): Balanced Nucleation and Growth, Most Widely Used Process Window
Medium heating rate retains part of the deformation driving force, the recrystallization nucleation density is moderate, the grain size is uniform and controllable, which is the conventional preferred parameter for tube furnace annealing.
Most tube furnace annealing processes adopt 2–10 ℃/min heating rate. It can avoid excessive recovery caused by too slow heating and uneven grain size caused by ultra-fast heating. The temperature gradient inside the sample is small, the thermal stress is low, and the risk of cracking of brittle ceramics is reduced. This interval is convenient for process adjustment: by matching different holding time, fine grain or medium grain structure can be obtained. It is widely used in stainless steel, aluminum alloy, alumina, zirconia and other material systems, and has good repeatability for batch production.
3.3 Fast / Ultra-Fast Heating Rate (>10 ℃/min): Suppress Recovery, High Nucleation Density, Obtain Fine Grains, Risk of Mixed Grains
Rapid heating skips the low-temperature recovery stage, retains high deformation storage energy, increases recrystallization nucleation rate, and obtains fine grains; but excessive heating rate easily causes temperature gradient and mixed grain structure.
Ultra-fast heating makes the sample quickly cross the recovery temperature range, the dislocation structure is retained, and the driving force for recrystallization is high. A large number of new crystal nuclei are formed instantaneously, and the grain growth time is insufficient, so the final grain is refined. This process is often used for fine-grained strengthening of metal alloys. However, too fast heating will bring obvious internal temperature gradient. The surface reaches the recrystallization temperature first, while the center is still in the recovery state. The difference of recrystallization sequence leads to mixed grain structure with large and small grains coexisting. For ceramics with poor thermal conductivity, rapid heating is easy to induce thermal stress cracking.
3.4 Slow Furnace Cooling: Sufficient Grain Growth, Low Residual Stress, Stable Equilibrium Microstructure
Slow cooling allows grains to continue to grow slightly in the high-temperature section, releases thermal stress, and obtains equilibrium phase and stable grain structure; it is suitable for stress-sensitive ceramics and brittle alloys.
Furnace cooling is the most common cooling mode of tube furnace annealing. After heat preservation, the power is cut off and the temperature drops naturally with the furnace. In the high-temperature slow cooling section, grain boundary diffusion continues, and the grains have a small amount of secondary growth. The temperature difference between the inside and outside of the sample is small, the thermal stress is released slowly, and the probability of cracking of ceramic samples is greatly reduced. The disadvantage is that for some metastable phase systems, slow cooling will induce phase transformation and change the grain structure formed at high temperature.
3.5 Controlled Medium Cooling Rate: Balance Stress and Grain Size, Convenient for Microstructure Locking
Programmed medium cooling can suppress excessive grain growth in the high-temperature zone, while avoiding excessive thermal shock, and is suitable for multi-stage annealing with strict grain size requirements.
By setting a fixed cooling rate of 1–5 ℃/min in the tube furnace program, the high-temperature grain structure can be quickly locked before the grain continues to grow. It avoids the long-time high-temperature residence of furnace cooling and prevents further grain coarsening. Combined with atmosphere protection, this method is widely used in functional ceramics, precision metal parts that require stable grain size and low residual stress.
3.6 Rapid Cooling / Gas Quenching: Suppress Grain Growth, Retain High-Temperature Microstructure, High Stress Risk
High-speed gas quenching rapidly passes through the high-temperature grain growth zone, freezes the grain state at the annealing temperature, and obtains fine grains; the temperature gradient is large, which is easy to introduce residual stress and cracks.
Tube furnaces equipped with rapid gas quenching function can inject high-flow protective gas to realize rapid cooling. The residence time in the high-temperature grain growth interval is extremely short, and the grain basically no longer grows during cooling, which can retain the fine grain structure formed at the annealing temperature. It is commonly used for metal alloys that need to retain high-temperature recrystallized structure. However, rapid cooling will produce huge temperature gradient inside thick samples. For ceramics, cermets and brittle materials, it is easy to crack. It is necessary to strictly control the gas flow rate and segment the cooling curve.
4. Material Classification and Process Parameter Matching Guide
4.1 Metal Materials (Alloy, Cold-Rolled Metal, Amorphous Alloy)
Fine-grained strengthening: inert / reducing atmosphere + fast heating + medium cooling; soft magnetic large grain: inert atmosphere + slow heating + furnace cooling; bright stress relief annealing: hydrogen reducing atmosphere + medium heating + slow cooling.
Cold-rolled aluminum alloy, copper alloy and stainless steel: if fine grain and high strength are required, adopt Ar atmosphere, heating rate 5–10 ℃/min, controlled cooling; if softening and high plasticity are required, slow heating 1–2 ℃/min and furnace cooling. Nickel-based alloy, high-temperature alloy bright annealing: dilute hydrogen argon mixed atmosphere, strictly control dew point, medium heating rate to avoid surface oxidation and abnormal grain growth. Amorphous alloy annealing: low vacuum or inert atmosphere, medium and low heating rate, avoid over-annealing crystallization and grain coarsening.
4.2 Oxide Ceramics (Al₂O₃, ZrO₂, BaTiO₃, YSZ)
Dense fine-grained ceramics: oxidizing / inert atmosphere + medium heating rate + slow cooling; reducing atmosphere annealing needs to shorten holding time to suppress abnormal grain growth.
Alumina, zirconia structural ceramics mostly adopt air or argon atmosphere, heating rate 1–5 ℃/min, furnace cooling, to obtain uniform grain and low stress. For dielectric ceramics such as barium titanate used in MLCC, reducing atmosphere is required for co-firing with nickel electrodes. At this time, the oxygen vacancy concentration rises, the grain growth is accelerated, and the holding time must be shortened to prevent individual grains from being abnormally large. Zirconia needs to control oxygen partial pressure to stabilize the tetragonal phase and avoid phase transformation and grain growth during cooling.
4.3 Non-Oxide Ceramics and Cermet (SiC, Si₃N₄, Metal-Ceramic Composite)
Non-oxide ceramics must use inert or vacuum atmosphere; reducing atmosphere should be used cautiously. Medium heating rate and segmented cooling are adopted to balance grain growth and anti-oxidation.
SiC and silicon nitride ceramics are easy to oxidize in air above 1000 ℃, so they must be annealed in high-purity argon or vacuum. The grain boundary is controlled by the sintering aid glass phase, and the heating rate cannot be too fast to prevent thermal cracking. For cermet such as Ni-YSZ, reducing atmosphere will promote the growth of metal phase particles and ceramic grains at the same time. The atmosphere oxygen partial pressure, temperature and holding time must be matched synchronously to avoid the mismatch of grain size between metal phase and ceramic phase.
5. Common Defect Troubleshooting and Annealing Curve Optimization
5.1 Mixed Grain, Abnormal Coarse Grain
Main causes: uneven heating rate, unstable atmosphere oxygen partial pressure, excessive holding time in reducing atmosphere; solutions: stabilize gas flow, reduce holding time, adopt segmented heating.
Mixed grains are one of the most common annealing defects. The root cause is the asynchronous recrystallization or uneven grain boundary migration rate. It is necessary to check whether the tube furnace has temperature gradient in the hot zone, whether the gas purging is sufficient before heating, and whether the hydrogen flow is too high. A segmented heating curve can be set: low-temperature preheating and heat preservation to homogenize the temperature field, then heat up to the target annealing temperature at a medium rate, and shorten the high-temperature holding time in reducing atmosphere.
5.2 Surface Oxidation, Discoloration and Grain Boundary Pollution
Main causes: insufficient purging, sealing leakage, residual oxygen in the tube; solutions: increase pre-purging time, check O-ring and flange sealing, use high-purity protective gas.
Even under inert gas, trace oxygen and water vapor will cause surface oxidation of metals and form impurity phases at ceramic grain boundaries, which will pin grain boundaries and make the grain size smaller than the expected value. Before annealing, the tube cavity needs to be purged for 3–5 times to replace the air. For high-demand bright annealing, a gas dew point detector is recommended to monitor the water vapor content in the atmosphere.
5.3 Thermal Stress Cracking of Ceramic Samples
Main causes: too fast heating or cooling rate, large sample thickness; solutions: add low-temperature preheating section, reduce ramp rate, avoid direct gas quenching of thick ceramic blanks.
Ceramic materials have low thermal conductivity and poor thermal shock resistance. Thick samples must be equipped with a long preheating section below 600 ℃ with a slow ramp rate. It is forbidden to directly use rapid gas quenching. If rapid cooling is required, segmented cooling is adopted: slow cooling in the high-temperature section above the phase transition point, and appropriately increase the cooling rate after the temperature drops to the low-temperature safe zone.
6. Summary and Process Design Suggestions
6.1 Core Law of Atmosphere and Ramp Rate on Grain Regulation
Atmosphere determines the diffusion driving force and grain boundary pinning state from the chemical level; ramp rate controls the recrystallization nucleation and grain growth time window from the kinetic level. The two are coupled together to determine the final grain structure.
Atmosphere is the chemical regulation knob of annealing: oxidizing atmosphere is easy to form pinning phase and refine grains; reducing / vacuum atmosphere increases vacancies, accelerates diffusion and promotes grain growth. The heating and cooling rate is the kinetic regulation knob: slow heating + slow cooling is conducive to grain growth and stress relief; fast heating + rapid cooling is conducive to grain refinement and locking high-temperature microstructure. There is no universal optimal parameter, and the material system and performance target must be the first priority.
6.2 Suggestions for Tube Furnace Annealing Process Development
When developing the annealing process, first lock the atmosphere according to the material anti-oxidation and phase stability requirements, then optimize the heating rate and holding time, and finally match the cooling curve.
The standard process development sequence is as follows: confirm the allowable atmosphere range of the material → set pre-purging parameters → formulate heating curve (preheating + formal heating) → determine annealing temperature and holding time → set cooling mode and cooling rate. For new materials, it is recommended to carry out gradient contrast experiments of atmosphere and ramp rate, and characterize the grain size by SEM / EBSD, so as to form a stable annealing process window. The multi-zone programmable tube furnace can realize more flexible segmented temperature and atmosphere switching, which is the preferred equipment for high-precision grain regulation.
Zhengzhou KJ Technology Co., Ltd. is a high-tech enterprise specializing in R&D and sales of heat treatment products, including muffle furnaces, tube furnaces, vacuum furnaces and more, widely used in metallurgy, ceramic sintering, battery materials, semiconductors, aerospace and other fields.
For inquiries and customized solutions, contact us via WhatsApp: +86 18037178440 or Email: web@kejiafurnace.com.